Goldlocks One‑Stop‑Solution: Connecting Global‑Farm‑Demand With Chinese‑Manufactured
Post‑Harvest‑&‑Smart‑Farming‑Machinery Snippet: As comprehensive Chinese agricultural‑machinery manufacturer,Goldlocks integrates potato‑sorting‑equipment, full‑set‑rice‑milling‑lines, grain‑processing‑machinery and intelligent‑agricultural‑robot‑system product‑portfolio. We deliver technical‑consulting, custom‑turn‑key‑project, strict‑quality‑controlled‑manufacturing and global‑after‑sales‑spare‑parts‑support. Our mission is supplying reliable‑farm‑equipment‑solutions for family‑farms, agricultural‑cooperatives and large‑smart‑agriculture‑projects all over the world.
Why ISO9001‑Certification Matters For International Agricultural‑Machinery Procurement For Overseas Farm‑Investors
ISO9001 quality‑management‑system‑certification represents standardized full‑process‑quality‑control for manufacturing‑enterprise. For overseas farm‑investors buying agricultural‑machinery from international‑supplier, ISO‑certification acts as important‑reference‑indicator for factory‑production‑management‑level. Goldlocks strictly follows ISO9001:2015 standard covering every production‑stage for potato‑processing‑machines, grain‑milling‑equipment and smart‑agricultural‑robots export‑orders.
Global‑Overseas‑Technical‑Support & Standardized‑Spare‑Parts‑Supply‑System For International Buyers
Core‑mechanical‑part quality determines farm‑equipment stability and service‑life. Goldlocks runs self‑owned CNC metal‑processing workshops to produce key mechanical‑components internally instead of fully outsourcing. In‑house machining capacity enables flexible modification for non‑standard custom‑project requirement and better delivery‑cycle control for overseas export orders.
Goldlocks accumulates more than 100 invention patents covering potato‑processing mechanical‑structure, grain‑processing innovation, AI‑vision grading algorithm and agricultural‑robot autonomous‑navigation‑technology. More than 59 professional engineers form the independent in‑house R&D team. Continuous technology‑innovation supports custom‑solution development for diversified global smart‑agriculture and post‑harvest‑processing projects.
For global farm investors, Goldlocks offers full turn‑key‑project service: site‑condition survey, production‑line‑process‑design, complete‑equipment‑matching, shipping‑arrangement, on‑site‑assembly guidance and local‑operator‑skill‑training. We handle projects for potato‑sorting plant, rice‑milling factory and smart‑robot‑unmanned‑farm construction. Customers receive one‑point technical support without coordinating multiple different‑suppliers.
Custom‑Turn‑Key‑Project Service Includes Process‑Design, Equipment‑Matching, Assembly‑Guidance And Operator‑Training
For global farm investors, Goldlocks offers full turn‑key‑project service: site‑condition survey, production‑line‑process‑design, complete‑equipment‑matching, shipping‑arrangement, on‑site‑assembly guidance and local‑operator‑skill‑training. We handle projects for potato‑sorting plant, rice‑milling factory and smart‑robot‑unmanned‑farm construction. Customers receive one‑point technical support without coordinating multiple different‑suppliers.
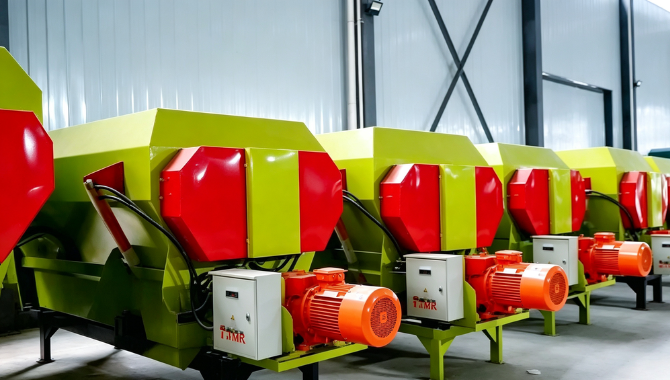
Medium‑size cattle‑raising cooperatives favor vertical‑structure TMR mixer for reliable mixing effect and relatively small‑footprint installation. Goldlocks vertical TMR mixer processes silage hay, grain feed and mineral additives into uniform mixed ration. Wear‑resistant mixing blades extend service‑life under heavy‑duty forage‑processing workload. Custom capacity models support different herd‑size requirements.
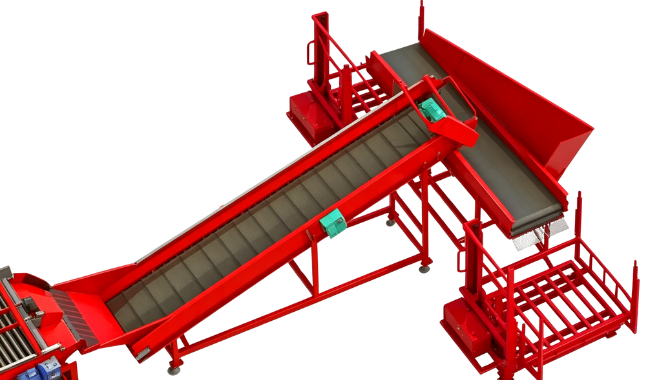
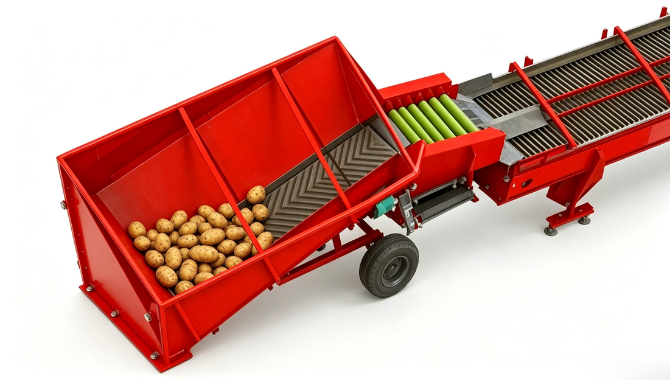
Goldlocks updates its potato post‑harvest portfolio with upgraded dry‑cleaning and mechanical grading equipment for medium‑large farms and food processors. The full‑line solution covers inbound receiving, soil removing, size grading, defect screening and automatic bagging. Built on ISO9001 production standards, these units reduce manual labor while boosting sorting consistency. Flexible layout design adapts to existing factory workshops. Global buyers can request turn‑key project consultation for potato warehousing‑unwarehousing sorting assembly lines.
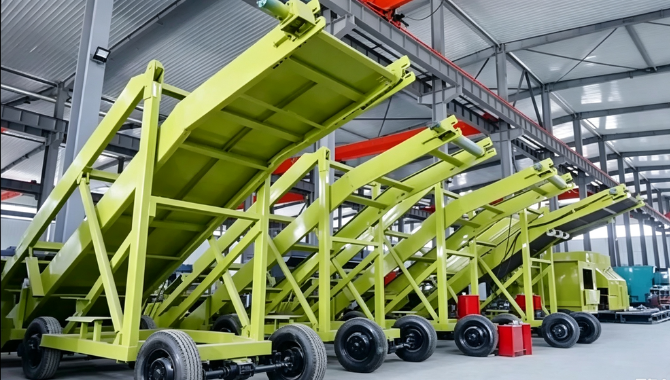
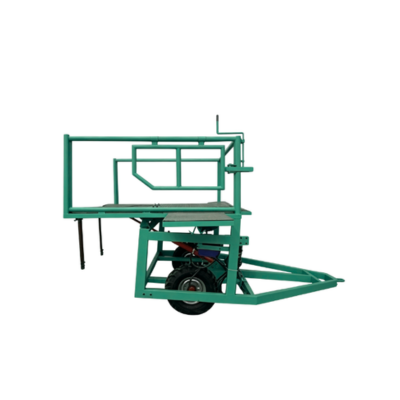
Silage fodder wagon completes field forage‑picking, chopping and transporting task for livestock‑raising bases. This farm‑machinery unit improves silage‑harvest workflow efficiency and reduces manual forage‑handling labor. Goldlocks silage‑fodder‑wagon matches well with silage‑loader and TMR mixer equipment to build complete forage‑processing production chain for cattle and sheep farms.
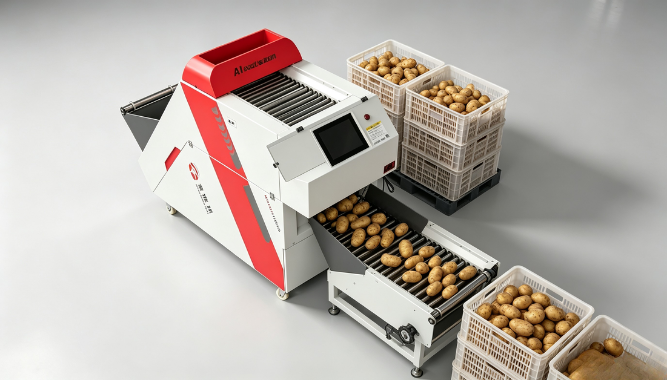
As labor shortages trouble many potato‑producing regions, AI‑powered vision counting equipment becomes a practical upgrade option. Goldlocks integrates self‑developed AI vision modules into potato washing‑sorting schemes, supporting multi‑grade classification for potatoes, sweet potatoes, carrots and onions. Every machine runs full‑load testing before shipment to cut on‑site debugging time. Custom ton‑bag and small‑bag automatic packing solutions are available for finished root‑crop products.

Many grain‑processing operators expand business into animal feed production. Goldlocks’s grain‑milling system realizes grain receiving, grinding, screening and automatic material discharging for livestock feed workshops. This mechanical set can work together with TMR mixer machines for dairy‑farm forage processing. Modular design allows adding or removing functional stations based on feed‑plant output target.
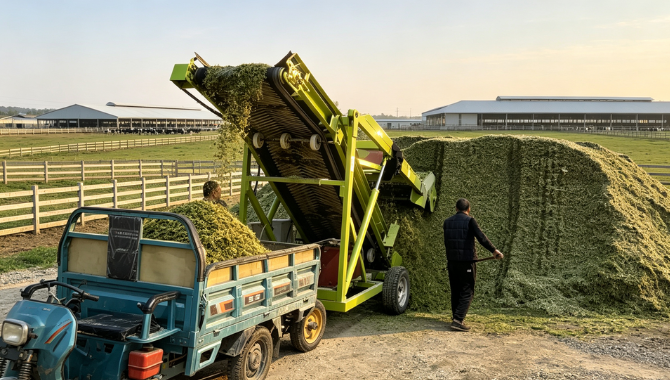
Labor cost pressure pushes livestock farms to adopt automated feeding equipment. Our electric cattle feeder delivers mixed TMR feed along cattle‑barn aisles automatically. Operators set feeding‑schedule via control panel instead of heavy manual fodder distribution. This equipment fits new‑build automated dairy‑barn renovation‑projects for global livestock customers.
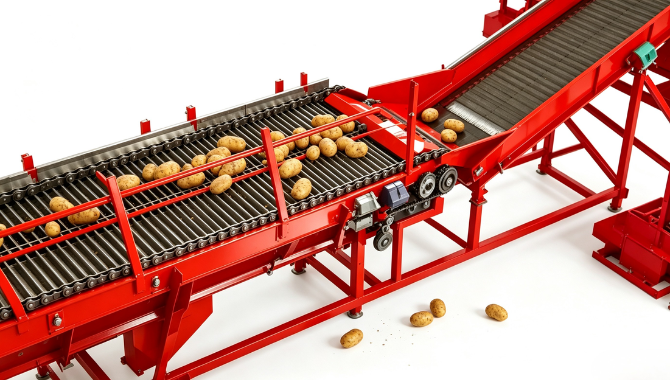
A leading agricultural cooperative in East Africa received a full set potato bagged‑storage production line from Goldlocks this quarter. This project includes washing, grading, conveying and automatic bagging units, designed for local high‑humidity planting conditions. Our engineering team provided site layout guidance and operator remote training. The ISO‑certified equipment helps local partners lower product loss rate during potato post‑harvest handling.
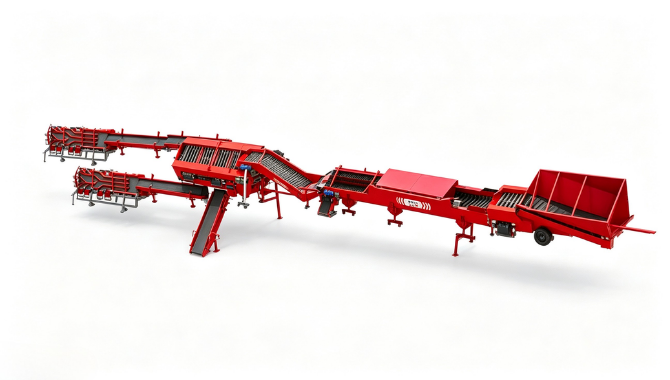
Many mid‑size potato processors prefer modular sorting lines instead of huge fixed installations. Goldlocks’s potato inbound‑outbound sorting production line supports phased capacity expansion: customers can add washing unit, optical sorter or bagging station later without rebuilding the whole workshop. CNC‑processed mechanical components guarantee long‑term running stability. Overseas spare‑parts supply system minimizes production downtime for global end‑users.
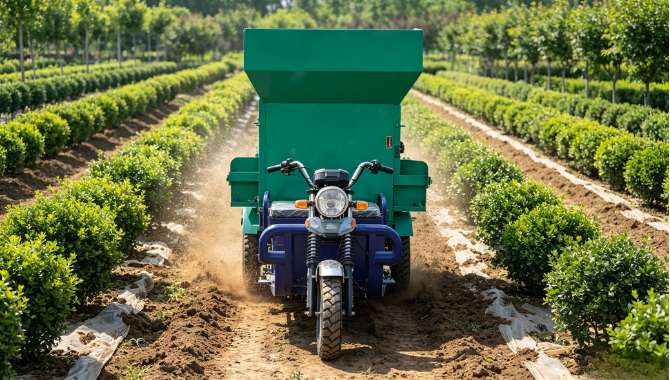
Silage‑material loading is heavy‑duty work inside forage‑processing zones.Goldlocks silage‑loader machine picks silage bales or bulk silage and feeds material into TMR mixer rapidly. Robust mechanical structure adapts for wet heavy silage raw‑material. It forms key auxiliary equipment for full‑set livestock‑feed‑preparation production line solution.
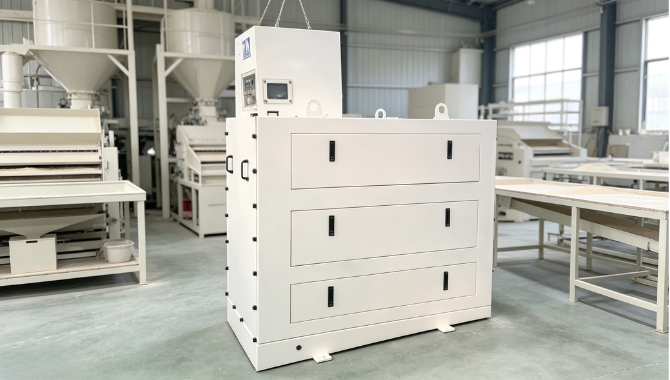
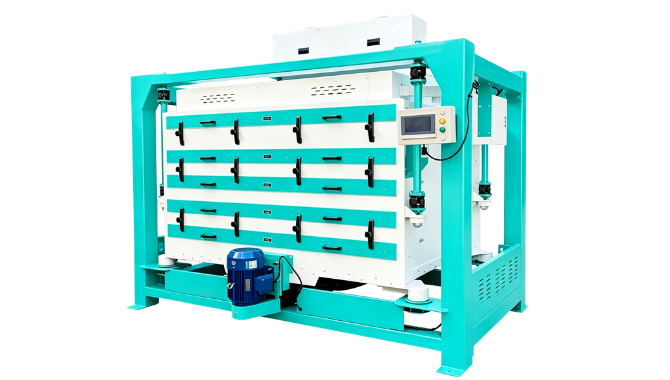
Whole‑rice yield directly decides rice‑mill project profit margin. Our gravity paddy separator and length‑thickness grader efficiently separate unhusked paddy from brown rice and classify kernel dimensions. Proper configuration of these core units reduces broken‑rice percentage during whitening and polishing phases. Goldlocks grain‑processing engineers provide parameter‑setting guidance for new rice‑plant operators.
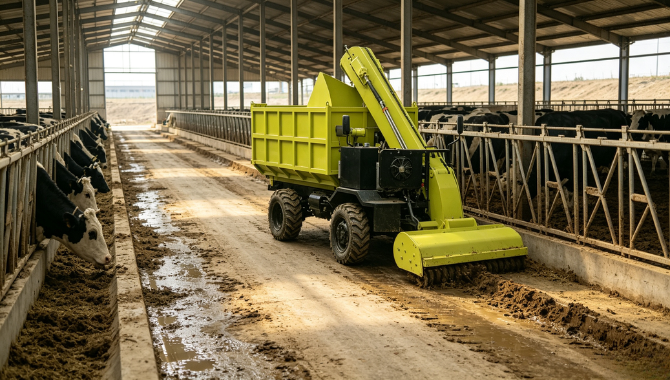
Manure‑cleaning consumes large‑volume manpower for large‑scale livestock barns. Goldlocks livestock barn cleaner executes automatic manure‑scraping along barn passageway. Regular automatic cleaning improves barn hygiene condition and lowers livestock‑disease risk. Different track‑layout configurations adapt for cattle‑barn, sheep‑house and mixed‑raising farm‑building structures.
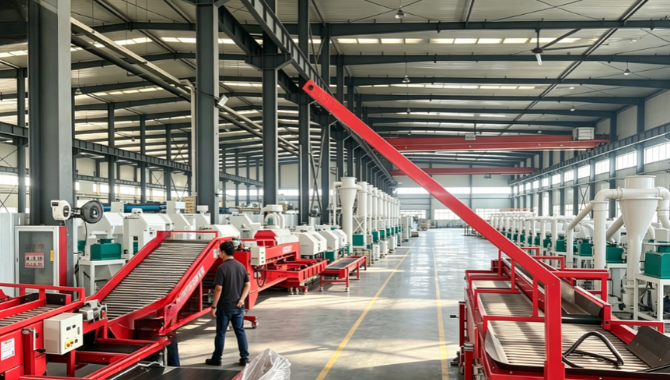
Uneven raw potato quality often disturbs post‑harvest workshops. Goldlocks releases its optimized Goldilocks potato washing‑sorting scheme, balancing cleaning intensity and tuber surface protection. The solution fits both fresh‑market potato packing and processing‑grade raw material pre‑treatment. Our R&D team adjusts water‑spray pressure, roller speed and grading threshold according to client sample tests. Custom layout drawings are offered for every inquiry.
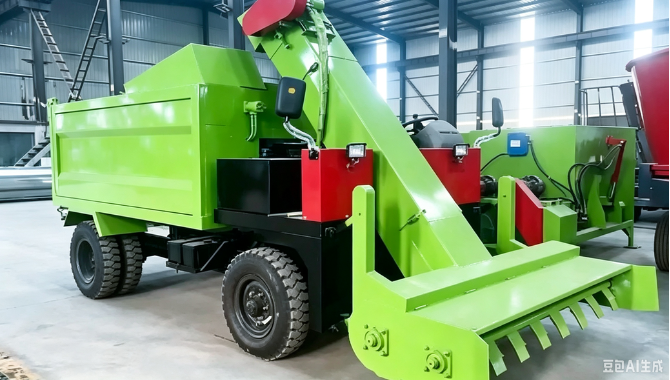
Modern circular‑agriculture requires proper farm‑manure collection and returning‑to‑field treatment. Our livestock waste tanker loads liquid manure from livestock barn and transports it for farm‑land fertilization application. This equipment helps livestock‑farm realize waste‑resource recycling and meets environmental‑protection‑management requirements for global agricultural‑production sites.

Existing rice mills often upgrade by adding optical sorting and automatic packing modules without rebuilding entire workshops. Goldlocks supplies standalone rice color‑sorter and bagging equipment for retrofitting projects. The optical sorter picks out discolored, diseased and defective rice kernels; automatic packer improves finished‑rice packing speed. Spare‑part kits and operation training are provided together with equipment delivery.
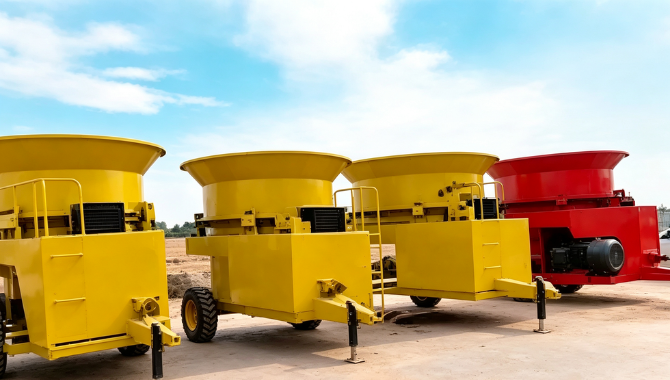
Many medium‑size livestock farms prefer grinding grain raw‑material on‑site instead of purchasing commercial finished feed. Goldlocks livestock feed grinder crushes corn, sorghum and other cereal grains for ration preparation. Working together with TMR mixing equipment, it realizes full‑process on‑farm feed processing for cattle‑raising cooperatives across emerging‑market regions.

Seed‑potato production demands precise sizing to guarantee seed quality. Goldlocks’s mini‑tuber sizing equipment serves seed‑potato research institutes and commercial seed farms. This mechanical grader separates seed tubers into multiple dimension classes without heavy surface damage. Combined with seed cleaner machines, it builds a complete seed pre‑processing workflow. Engineers provide technical support for secondary configuration adjustment.
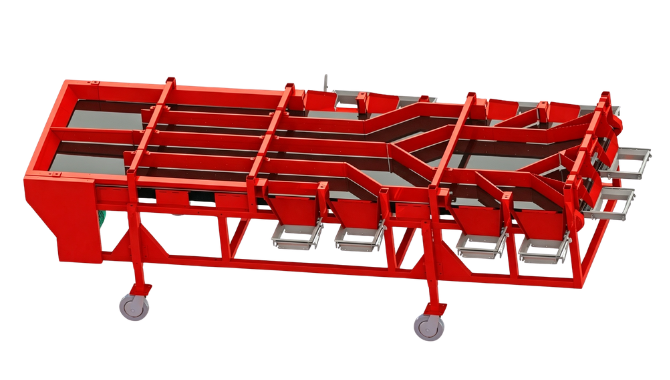
South American potato packers face rising manual‑recruitment costs. Our standalone automatic bagging machine matches perfectly with existing potato sorting lines, realizing semi‑automatic finished‑product packing. Operators only supervise the running status instead of heavy‑duty bag‑filling work. The equipment supports ton‑bag and woven small‑bag switching. Goldlocks supplies full spare‑part kits along with each machine export order.
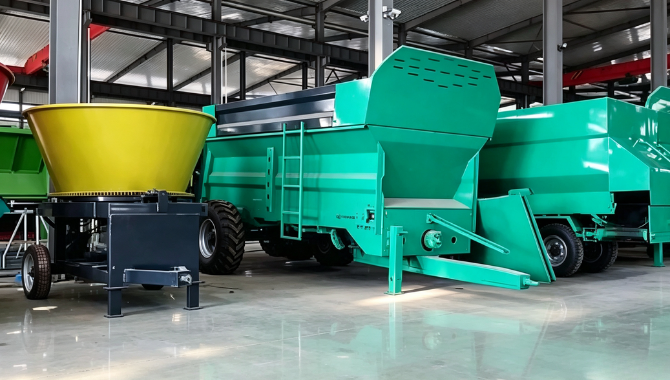
Goldlocks provides one‑stop livestock‑forage‑processing turn‑key solution including silage loader, fodder wagon, TMR mixer, livestock barn cleaner and waste‑tanker. Our engineering team evaluates herd‑scale, barn‑layout and local forage‑supply condition before equipment matching. The integrated solution serves dairy‑farm, beef‑cattle‑raising cooperative and large‑scale sheep‑farm investors globally.
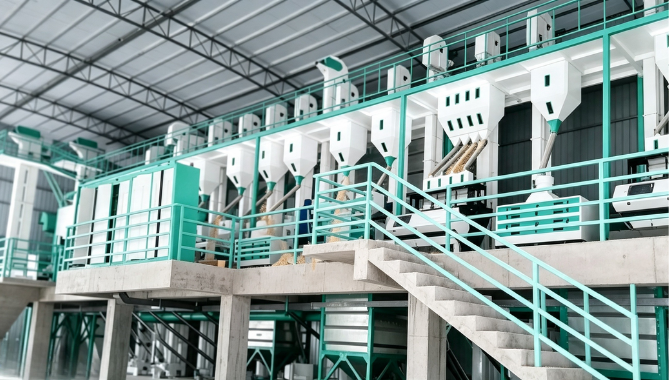
Food‑processing factories handle rice, corn, soybean and spice raw materials at different periods. Goldlocks multi‑function grain‑processing equipment supports rice milling, corn grinding, soybean pulping as well as spices grinding work. Quick‑change screen and roller groups realize crop‑switching without large‑scale reconstruction. This multi‑purpose setup helps processors improve equipment utilization rate.
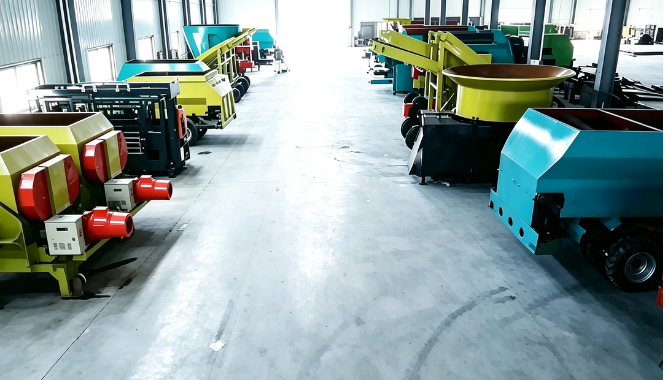
Livestock‑raising workshops run year‑round; unexpected machine‑breakdown brings serious feeding‑schedule risk. Goldlocks maintains dedicated spare‑parts inventory for TMR mixers, silage‑loaders and barn‑cleaning equipment. Fast‑logistics spare‑part delivery plus remote‑maintenance guidance support overseas livestock‑farm customers to minimize equipment‑downtime risk.
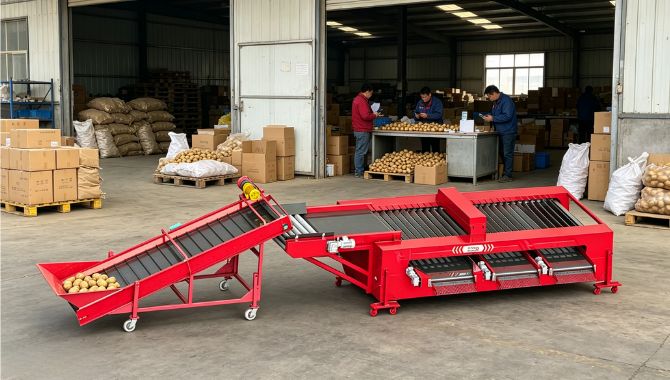
Raw‑material selection, welding standard and component assembly directly decide farm machinery service cycles.Goldlocks strictly follows ISO9001:2015 quality rules during potato processing equipment production. Raw metal cutting, welding and component assembling are operated inside separated standardized workshops. Every finished grader must finish full‑load running inspection before container loading to avoid early‑stage failure after arrival.
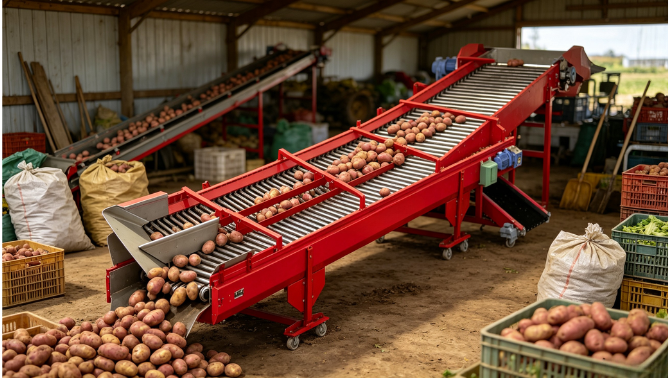
More global farm investors tend to select one‑stop root‑crop solutions instead of scattered single machines. Goldlocks supplies complete workflows from field potato digging, in‑farm conveying, washing grading all the way to warehouse storage system. Project teams finish process design, equipment matching and assembly guidance for overseas clients. Solutions cover potato, sweet potato, carrot, onion and sugar‑beet processing scenarios.
Global specialty‑grain market for sorghum and millet keeps expanding. Goldlocks designs dedicated processing workflows including cleaning, husking, whitening, grading and packaging for sorghum and millet. The machinery adjusts processing intensity to avoid kernel over‑breakage. Multiple capacity options fit small artisan workshop and large‑scale industrial specialty‑grain plant.
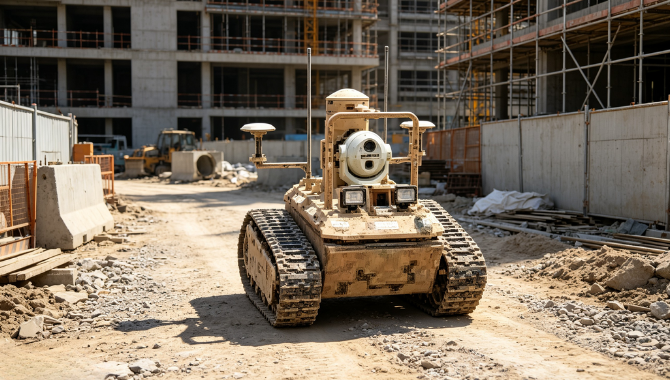
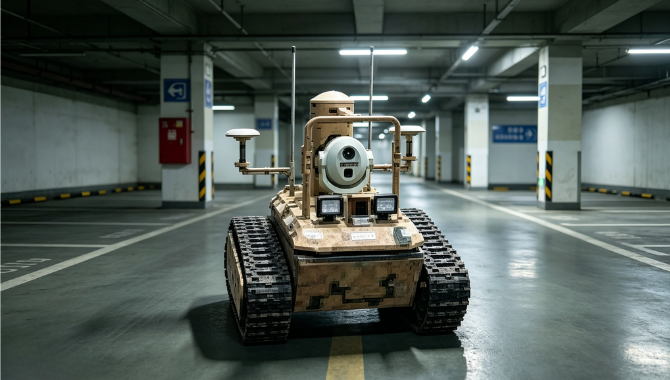
Many farm sites own sloped ground and muddy soil after rainfall, restricting wheeled‑robot movement. Crawler‑type inspection robot from Goldlocks adopts tracked walking structure for complex off‑road farm terrain. It carries cameras and environment‑sensors to finish mobile‑monitoring task in orchard, open‑field crop area and silage‑storage zones. Custom payload‑mounting service is available for project‑specific requirements.
Bulk stored potatoes need re‑grading before entering sales channels. Goldlocks’s potato warehousing‑unwarehousing sorting assembly line handles stock material unloading, impurity removing, re‑sizing and diverting. This line reduces heavy manual handling inside cold‑storage warehouses. Clients can choose to add AI vision defect‑inspection modules as optional upgrades. Flexible MOQ accepts both single‑unit and full‑line purchase requests.
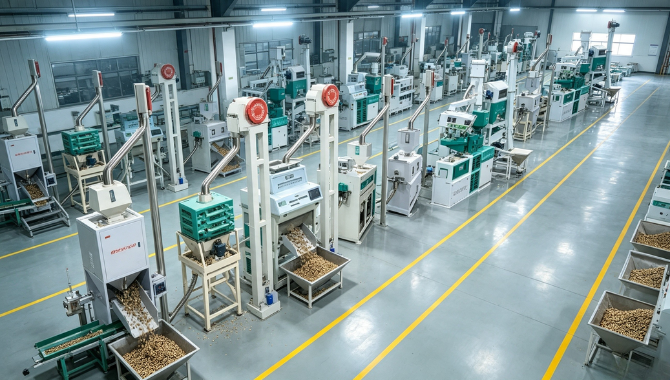
An agricultural cooperative in Africa chose modular rice‑milling units from Goldlocks for local grain‑processing modernization. Comparing multiple international suppliers, the client valued our ISO9001 quality certification, rich overseas‑project references and factory‑direct pricing advantage. Our team completed process planning and operator training. Local farmers now obtain higher‑value finished‑rice products locally instead of importing milled rice.
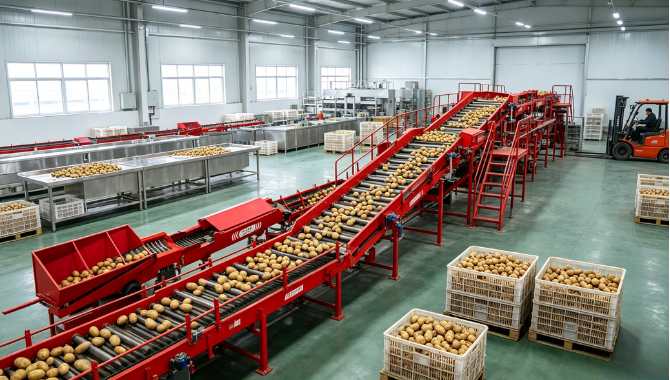
A large potato farm in Central Asia replaced its outdated manual sorting workshop with Goldlocks’s mechanical potato graders this year. After installation, hourly processing capacity increased greatly while product damage rate dropped obviously. Our overseas technical team provided remote video guidance for machine assembling and parameter tuning. Local agricultural cooperatives now reference this project for their own modernization plans.
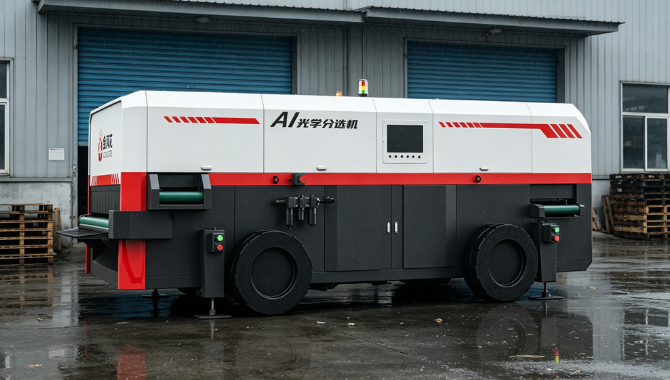
Goldlocks maintains an in‑house R&D team with over 59 engineers covering mechanical‑structure, AI‑vision grading and robot‑navigation‑algorithm research. All core navigation and vision software are self‑developed instead of full‑external sourcing. We hold more than 100 invention patents for agricultural machinery and robot technologies. Independent R&D capacity supports fast custom modification for overseas smart‑agriculture project requirements.
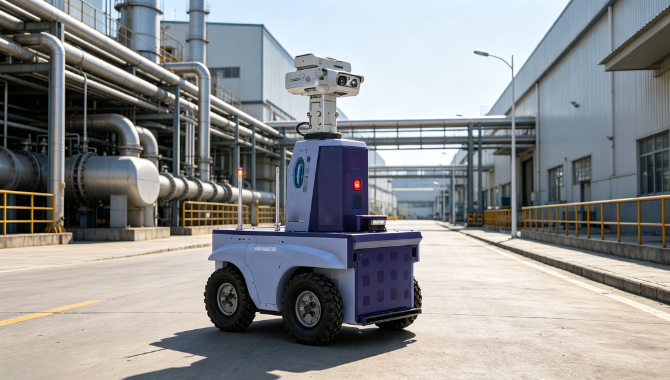
Certain grain‑warehouse and agricultural‑processing industrial zones require explosion‑proof mobile‑robot equipment. Goldlocks intelligent explosion‑proof lifting inspection robot meets explosion‑safety standards for high‑risk working zones. Lifting mechanism expands sensor observation height; autonomous navigation guarantees flexible patrol. This product receives inquiry from grain‑storage management institutes and industrial‑park clients globally.
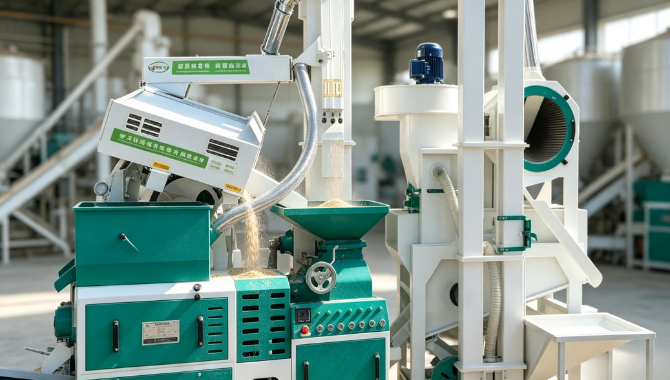
High broken‑rice rate seriously lowers rice‑mill economic returns. Multiple factors affect kernel integrity: paddy moisture input, machine gap setting, feeding speed and component wear status. Goldlocks grain‑processing engineers summarize practical operation tips for global rice‑plant customers. We deliver technical documents and remote video guidance helping operators adjust whitener, husker and separator parameters correctly.
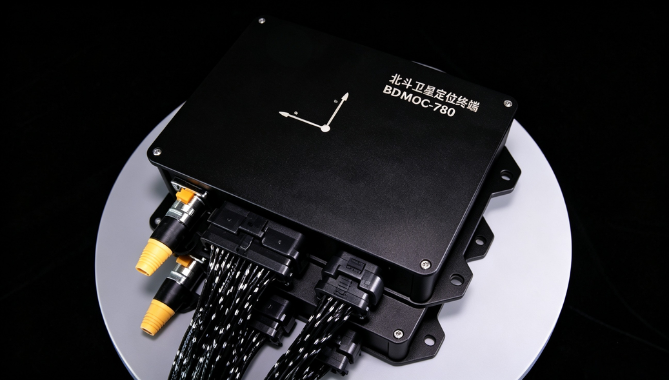
One agricultural‑research institute from India purchased Goldlocks Beidou RTK navigation controller plus explosion‑proof mobile chassis for local agricultural‑robot development project. The client set strict standards for positioning precision, environmental adaptability and secondary‑development compatibility. Our engineering team delivered SDK documents and technical consultation supporting the institute’s robot‑prototype development work.
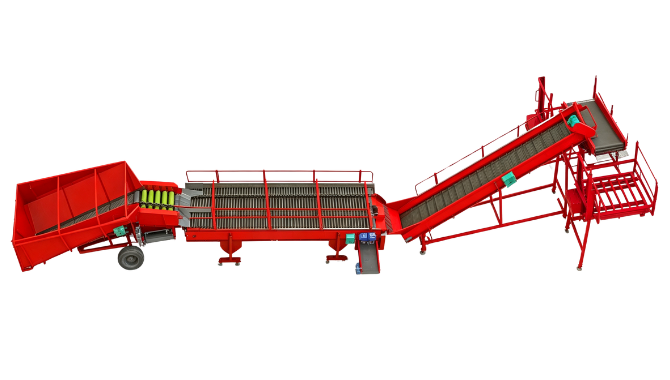
A large potato farm in Central Asia replaced its outdated manual sorting workshop with Goldlocks’s mechanical potato graders this year. After installation, hourly processing capacity increased greatly while product damage rate dropped obviously. Our overseas technical team provided remote video guidance for machine assembling and parameter tuning. Local agricultural cooperatives now reference this project for their own modernization plans.
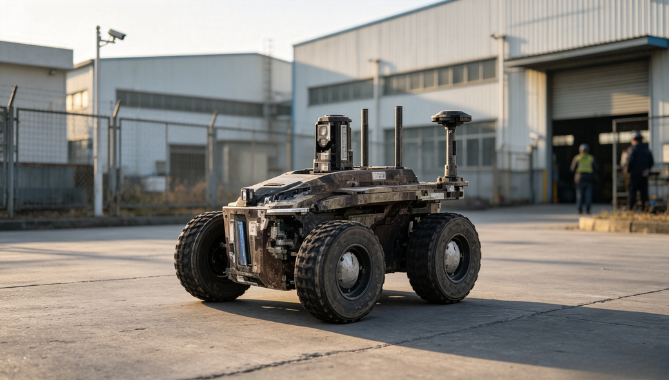
Modern smart‑farm and agricultural‑park need mobile inspection robots to patrol greenhouse, barn and field‑facility sites. Our wheeled inspection robot carries multi‑functional sensor payload for environment‑data collection and video surveillance. Based on modular robot‑chassis and Beidou RTK navigation, it moves along pre‑set patrol routes automatically. Secondary‑development API is provided for system integrator partners.
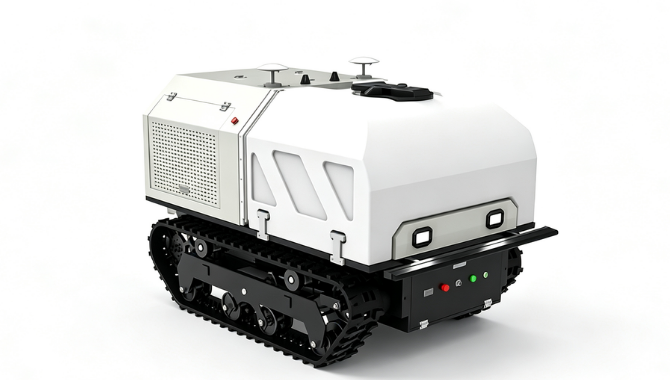
Every smart‑agricultural robot unit undergoes complete in‑house inspection before shipment: navigation‑position accuracy test, obstacle‑avoidance simulation, full‑load continuous‑running and payload‑driving verification. Our QC technicians record all test‑parameter logs. Strict pre‑shipment testing reduces unexpected faults after robot arrives at overseas customer farm sites.

Reliable rice‑milling performance starts from incoming‑component quality control. Under ISO9001:2015 management rules, Goldlocks inspects raw metal material, motor units, bearing parts and wear‑resistant rollers before grain‑machine assembly. Unqualified spare parts get eliminated before entering production workshops. Each finished rice‑milling unit must run full‑load test before export shipment.
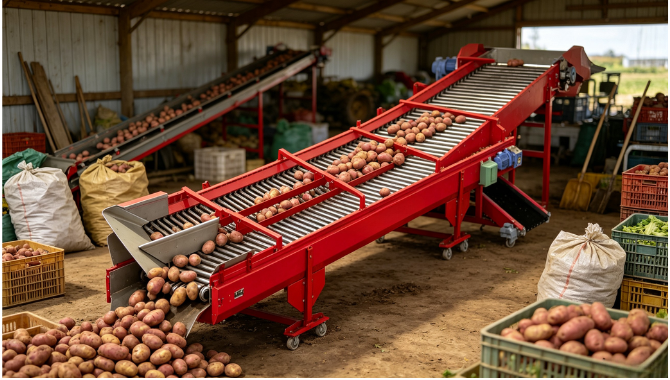
Food‑safety regulations push global potato packers to adopt food‑grade stainless‑steel processing equipment. Goldlocks builds core contact parts of washing and sorting machines with qualified stainless‑steel material. Anti‑corrosion design suits humid cleaning workshops. We accept third‑party factory inspection before shipment for big‑volume potato‑line export contracts.
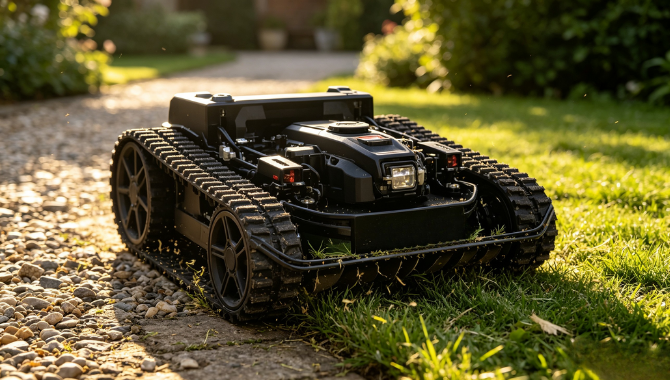
Different smart‑farm projects require different robot working functions. Goldlocks provides custom software‑hardware configuration service for agricultural robots: clients may add polishing module, color‑sorting payload, spray‑unit or special‑task sensor kit. Our R&D team adjusts control‑software logic matching newly‑installed implements. Non‑standard automation modification supports special‑scenario smart‑agriculture project demands.
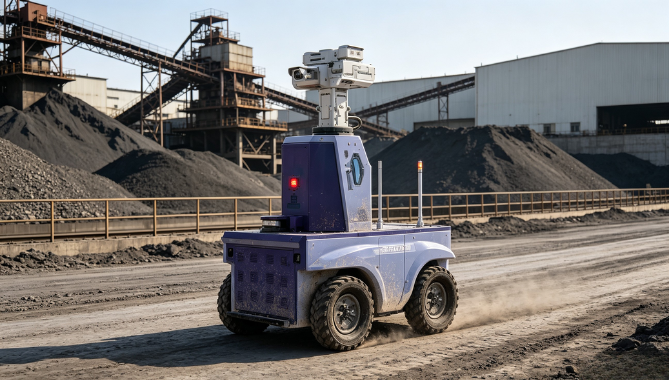
Certain grain‑warehouse and agricultural‑processing industrial zones require explosion‑proof mobile‑robot equipment. Goldlocks intelligent explosion‑proof lifting inspection robot meets explosion‑safety standards for high‑risk working zones. Lifting mechanism expands sensor observation height; autonomous navigation guarantees flexible patrol. This product receives inquiry from grain‑storage management institutes and industrial‑park clients globally.
After agricultural‑robot delivery, remote‑management capability is critical for overseas users. Goldlocks robot system reserves remote‑access function: authorized technicians can check robot operation log, adjust navigation‑parameter and diagnose software‑related faults remotely. Combined with spare‑parts fast‑supply system, it forms complete after‑sales support for international smart‑agriculture buyers.
Many existing farm buildings have restricted floor area and height, limiting new processing‑line installation. Goldlocks engineering department draws custom production‑line layout drawings according to client‑supplied plant dimension data. We rearrange conveyor angle, machine sequence and transfer‑point positions to match on‑site conditions. Non‑standard automation modification service is available for special‑requirement potato projects.
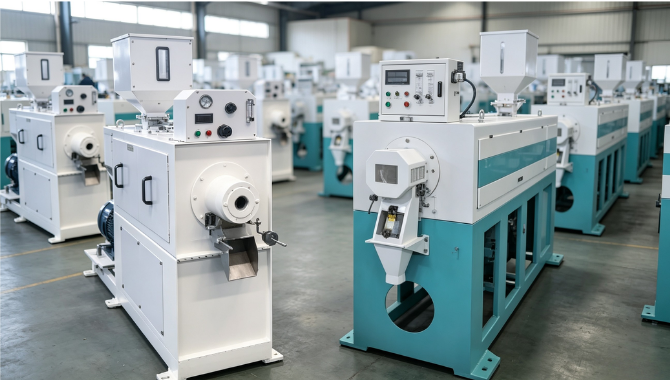
New market entrants look for low‑threshold mini rice‑mill turn‑key solutions. Goldlocks provides compact combined rice‑milling unit plus supporting conveyor, elevator and small‑packing machine for startup projects. Lower total investment, simplified operation and smaller workshop‑space requirement make it fit family‑run agricultural enterprises. Flexible MOQ accepts single‑set mini‑mill purchase order.
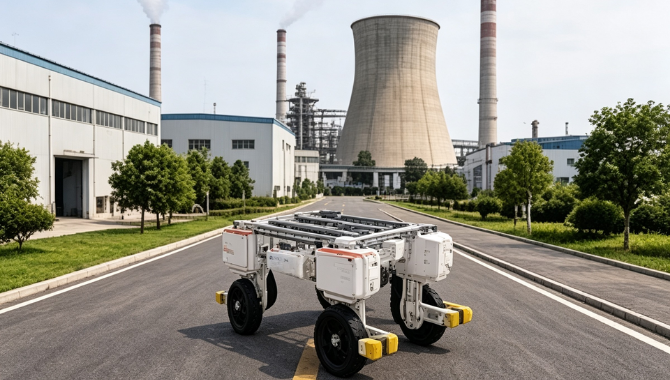
Building smart‑agriculture pilot projects from scratch costs huge R&D budget. Adopting mature modular agricultural‑robot chassis as mobile platform greatly cuts development cycle and hardware‑investment. Goldlocks chassis provides stable mobility system; project teams only focus on developing their own upper‑mount business‑function payload. This solution gains popularity among agricultural‑universities and tech‑start‑ups.
Remote planting bases without stable grid power need special‑adapted post‑harvest machinery. Goldlocks offers hybrid‑power auxiliary modules for potato washing‑sorting production lines. Diesel‑electric hybrid configurations help equipment keep normal operation where mains electricity supply is unstable. This solution wins positive feedback from remote mountain‑area root‑crop farms across Southeast Asia.
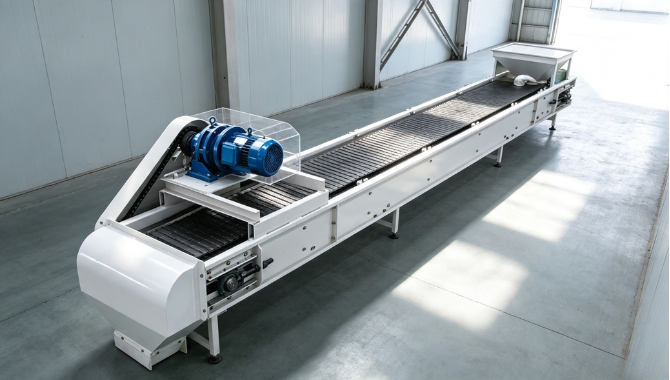
Smooth material transportation avoids grain crushing and production‑line bottlenecks. Goldlocks supplies complete series of bucket elevators, belt conveyors and screw conveyors matching rice‑milling workflows. Wear‑resistant structural parts extend service life under continuous grain‑handling workload. Custom length and inclination angle satisfy different rice‑plant site layout needs worldwide.
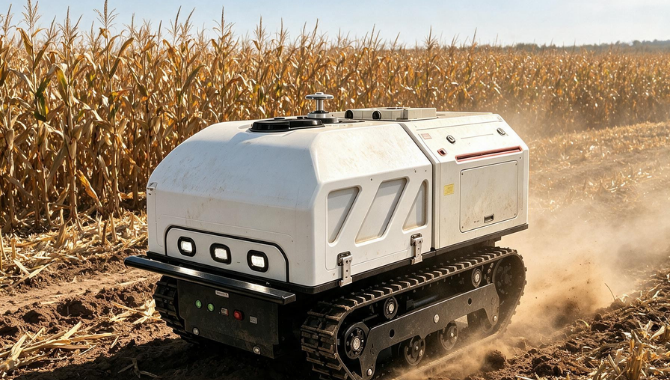
Hilly orchard regions face serious plant‑protection‑worker shortage, raising fruit‑production cost year‑by‑year. Autonomous orchard spray robot works day‑shift without heavy‑labor requirement. Beidou RTK keeps precise driving path even on slope terrain. Goldlocks accumulated multiple orchard‑robot pilot‑project cases for reference by global fruit‑farm investors.
Many farm sites own sloped ground and muddy soil after rainfall, restricting wheeled‑robot movement. Crawler‑type inspection robot from Goldlocks adopts tracked walking structure for complex off‑road farm terrain. It carries cameras and environment‑sensors to finish mobile‑monitoring task in orchard, open‑field crop area and silage‑storage zones. Custom payload‑mounting service is available for project‑specific requirements.
Before buying agricultural robot equipment, farm operators need to assess positioning accuracy, terrain adaptability, payload‑capacity, working endurance, after‑sales‑support and secondary‑expandability. Goldlocks smart‑agriculture consultants help overseas customers analyze real‑field working‑condition and match suitable robot‑model for orchard, pasture or crop‑field scenarios.
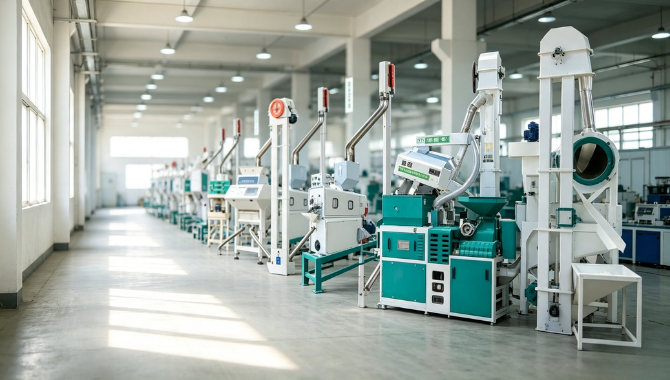
A rice‑processing plant operator based in Laos completed commissioning of Goldlocks’s full‑set 20‑25t/d rice milling line. The integrated workflow covers rice cleaning, destoning, husking, separation, whitening, polishing, optical sorting and final packaging. This turn‑key project helped the customer reduce broken‑rice rate and lower frequent‑downtime trouble from old‑generation equipment. Remote after‑sales support continues to guarantee stable daily production.
Inside Goldlocks factory, independent robot‑algorithm‑debugging lab simulates various farm‑field interference conditions to test navigation controller performance. Engineers tune path‑planning and obstacle‑avoidance algorithm repeatedly before mass‑production. Laboratory verification minimizes risk when robots run under real‑world complex outdoor farm‑environment in different countries.
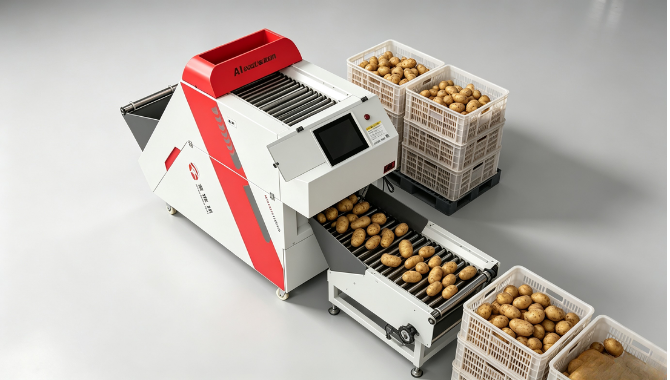
Instead of purchasing brand‑new whole lines, many processors choose to retrofit AI vision inspection onto current potato grading equipment.Goldlocks provides vision‑module retrofit service for compatible sorting machines. After upgrading, the system automatically identifies bruises, green skin, rot and surface cracks on tubers. Remote software iteration keeps vision‑recognition algorithms updated without hardware replacement.
Global smart‑agriculture investment keeps rising; farms and agricultural‑cooperatives seek affordable unmanned‑robot solutions. Chinese manufacturers bring competitive‑priced Beidou‑navigation‑based agricultural‑robot products to international market. Goldlocks receives increasing inquiries for orchard‑robot, mowing‑robot and modular‑chassis export orders across Asia, Africa and Latin‑America regions.
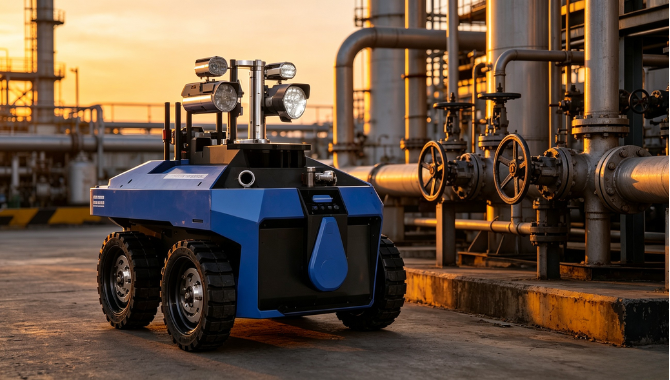
Certain grain‑warehouse and agricultural‑processing industrial zones require explosion‑proof mobile‑robot equipment. Goldlocks intelligent explosion‑proof lifting inspection robot meets explosion‑safety standards for high‑risk working zones. Lifting mechanism expands sensor observation height; autonomous navigation guarantees flexible patrol. This product receives inquiry from grain‑storage management institutes and industrial‑park clients globally.
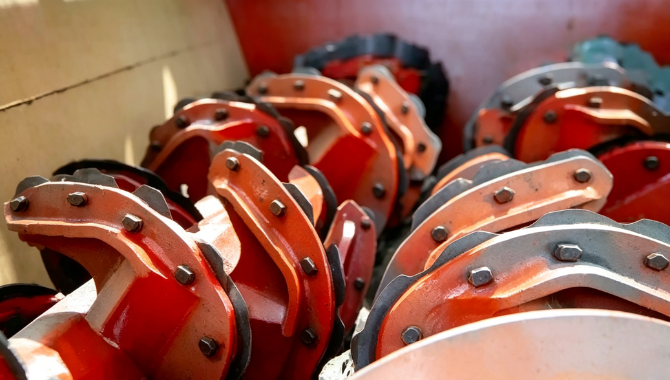
Accurate total‑mixed‑ration preparation is essential for dairy‑cow raising performance. Goldlocks TMR preparation machine mixes silage, grain concentrate and additive evenly for livestock barns. Vertical TMR mixer and horizontal‑type models are both available for different‑scale dairy‑farm projects. We supply matching silage‑loader machine together for complete forage‑handling workflow.
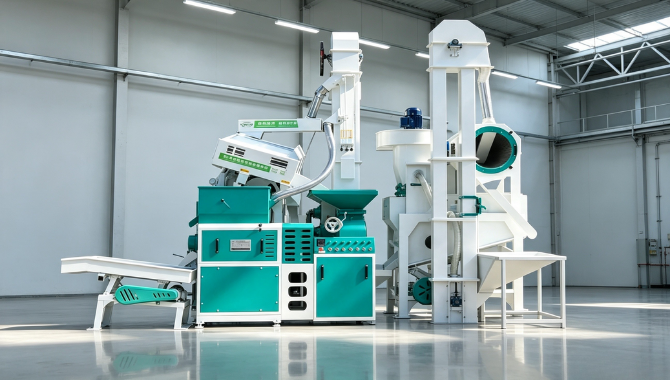
Beyond cereal grain processing, our grinding‑mill platform adapts for spices, coffee and cocoa raw‑material fine‑grinding. Goldlocks configures different grinding‑roller assemblies for oily or fibrous spice raw materials. Food‑grade stainless‑steel contact‑parts meet food‑hygiene requirement for spice‑processing workshops. We support custom grinding‑fineness parameter setup according buyer sample test.
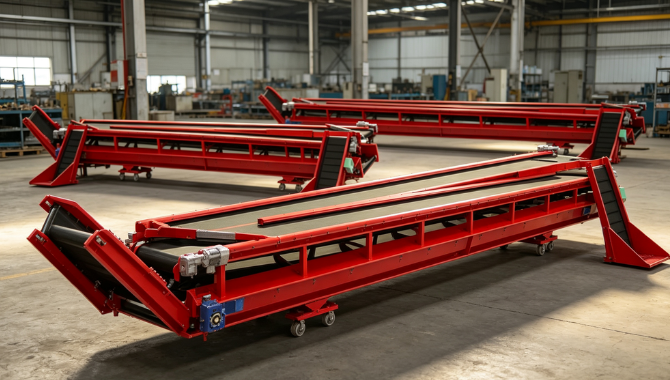
Fast spare‑part delivery is critical for year‑round potato‑processing workshops. Goldlocks maintains standardized spare‑parts inventory system for all potato‑series machinery. After‑sales team sends operation manuals, maintenance videos and arranges fast‑logistics component delivery for international buyers. Remote troubleshooting supports customers to resolve minor faults without on‑site technician arrival.
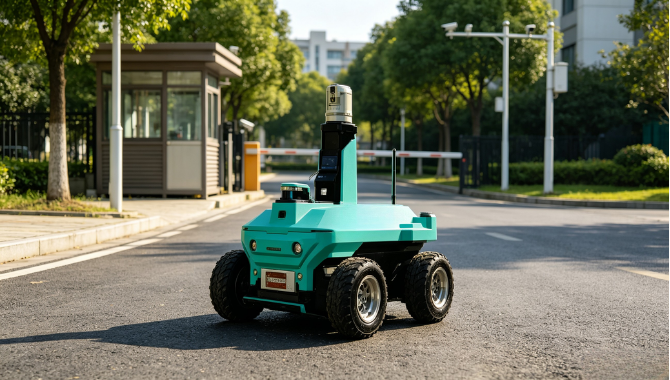
Modern smart‑farm and agricultural‑park need mobile inspection robots to patrol greenhouse, barn and field‑facility sites. Our wheeled inspection robot carries multi‑functional sensor payload for environment‑data collection and video surveillance. Based on modular robot‑chassis and Beidou RTK navigation, it moves along pre‑set patrol routes automatically. Secondary‑development API is provided for system integrator partners.
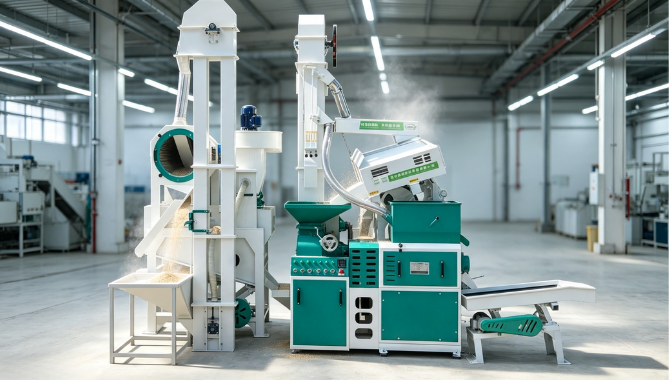
For mid‑size agricultural cooperatives, compact combined rice milling units bring balanced capacity and capital investment. Goldlocks’s combined rice‑milling machine integrates multiple grain‑processing functions inside one unit. Clients can add separate polisher or color‑sorter modules later as business expands. Factory pre‑assembly shortens field installation cycles for overseas rice‑mill projects.
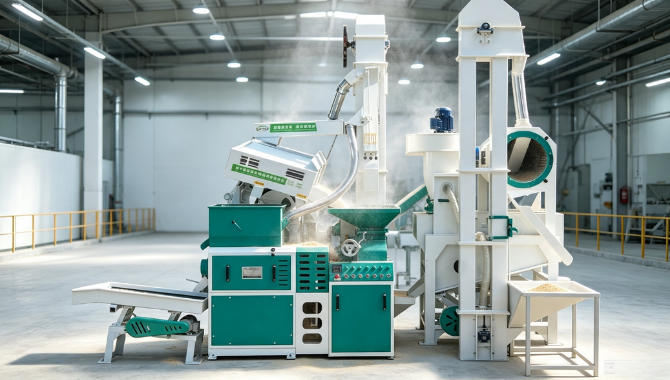
Time‑zone difference and long transportation distance bring challenges for overseas grain‑plant maintenance. Goldlocks’s grain‑processing after‑sales department provides remote video troubleshooting for international rice‑mill customers. Machine operation manuals, maintenance check‑lists and fault‑diagnosis documents get delivered with each equipment shipment. Spare‑parts logistics system shortens component‑replacement waiting periods.
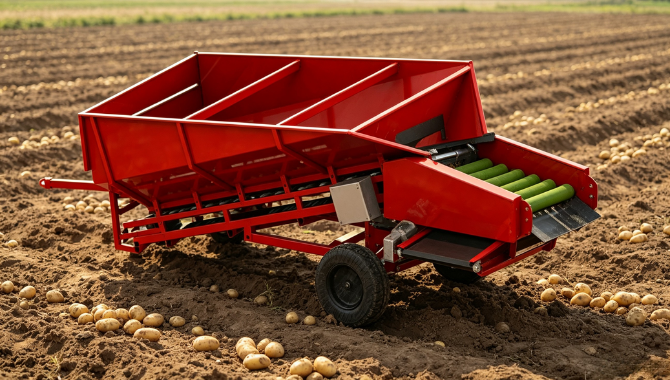
Planning a potato post‑harvest project requires evaluation on hourly capacity, raw‑material varieties, workshop space, power supply and final‑product destination. Goldlocks technical consultants help global customers sort out key indexes before formal quotation. We compare modular scheme versus integrated fixed‑line scheme according to farm scale: family farm, medium cooperative and large industrial plant get differentiated equipment proposals.
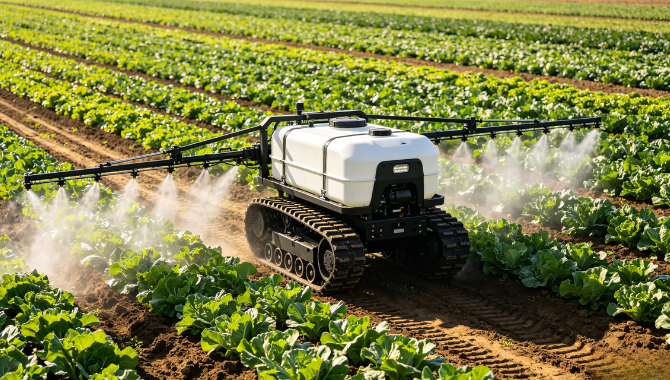
Pure‑electric farm robots are limited by battery endurance for large‑area field operation. Goldlocks hybrid‑power farm spray robot combines internal‑combustion power generation and electric‑drive walking system. This hybrid setup supports long‑time continuous plant‑protection spraying for crop fields. Remote monitoring function lets operators check robot working status from control terminal.
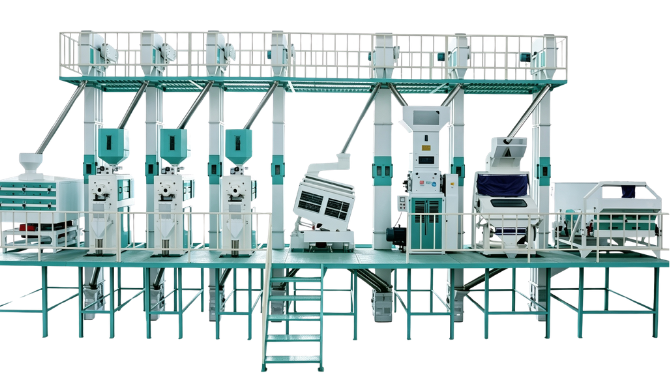
Selecting suitable hourly‑throughput is vital for rice‑mill investment return. Goldlocks sorts capacity‑selection reference for global investors: 5‑10t/d for small cooperative; 15‑25t/d for mid‑size plant; 30‑50t/d for large industrial rice‑processing factory. Our technical team evaluates local paddy supply volume, working‑shift arrangement and finished‑rice sales volume before recommending equipment specifications.
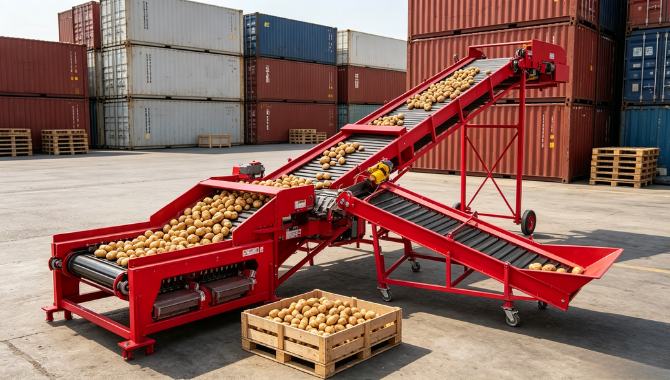
Diversified farms process multiple root‑crops: potato, sweet potato, carrot and onion in different harvest seasons. Our shared‑use washing‑grading equipment realizes quick roller and sieve‑size switching for different tuber types. One set of machinery serves multi‑crop post‑harvest demands and cuts total equipment investment cost for agricultural cooperatives.
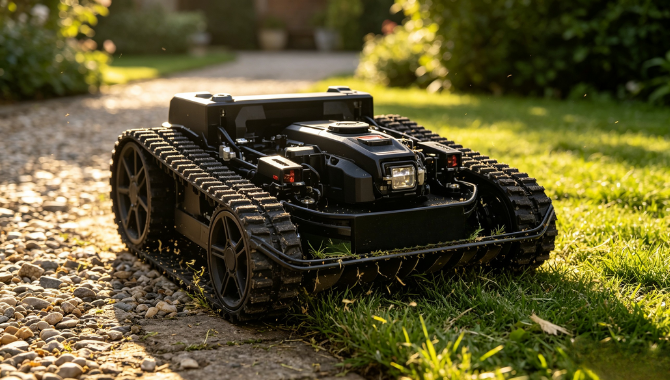
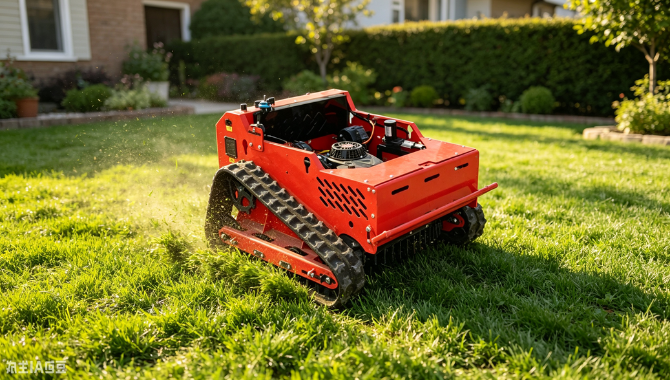
Farm pasture maintenance and orchard inter‑row grass‑removal consume plenty manpower. GL‑G800 navigation lawn‑mowing robot executes autonomous mowing mission with Beidou‑based path navigation. Obstacle‑avoidance sensor system guarantees safe running under complex field‑environment. Farmers define working‑area boundary via software; robot finishes mowing task without continuous human supervision.
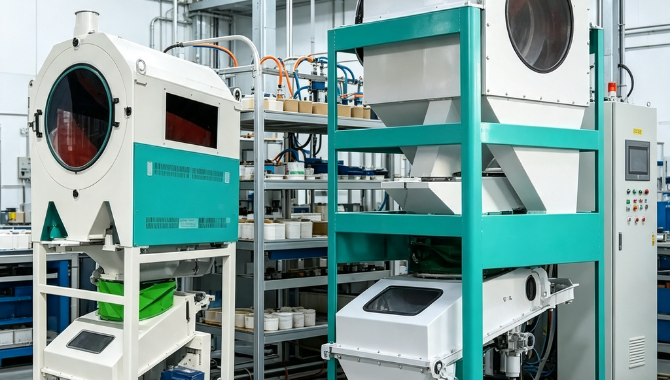
Stones, sand and heavy impurities mixed inside incoming paddy will accelerate husker and whitener component wear. Installing high‑performance pre‑cleaning and destoning unit at production‑line front‑end effectively protects expensive downstream rice‑milling equipment. Goldlocks integrates heavy‑impurity removal module for both standalone unit and full rice‑milling turn‑key lines.
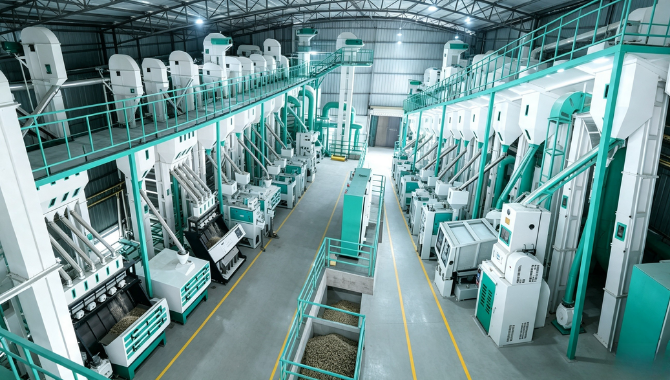
Goldlocks delivers end‑to‑end rice‑processing plant solutions: technical consulting, site layout drawing, complete‑set equipment, shipping arrangement plus overseas installation guidance. The whole‑line includes paddy cleaner, gravity paddy separator, length‑thickness grader, rice whitener, polisher, optical sorter, elevator‑conveyor and automatic packing machine. Solutions adapt for small family mill up to large industrial rice‑processing factory.

Manual weighing‑and‑bagging brings measurement deviation and low efficiency for rice‑processing plants. Goldlocks automatic grain‑packing machine finishes feeding, weighing and bag‑sealing automatically. Built‑in weight‑checking module rejects out‑of‑tolerance packages. The unit can connect directly with rice‑optical‑sorter output outlet to realize continuous finished‑rice packing workflow.
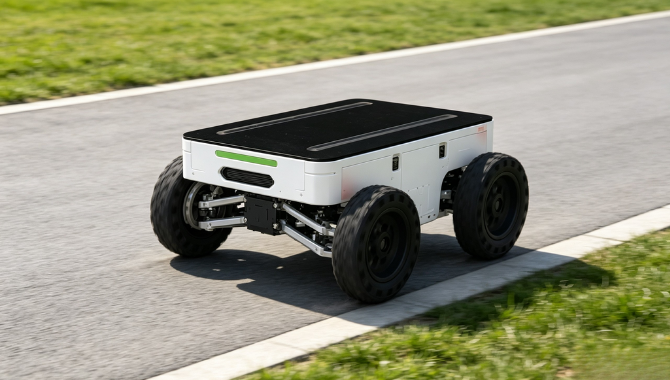
Modular robot‑chassis platform lowers development threshold for diversified smart‑agriculture applications. Goldlocks agricultural robot chassis reserves standard mounting interfaces: users can install spray module, mowing unit, inspection sensor or fertilizer‑spreading device without redesigning mobility system. This hardware suits agricultural‑robot research projects as well as commercial unmanned‑farm deployment.
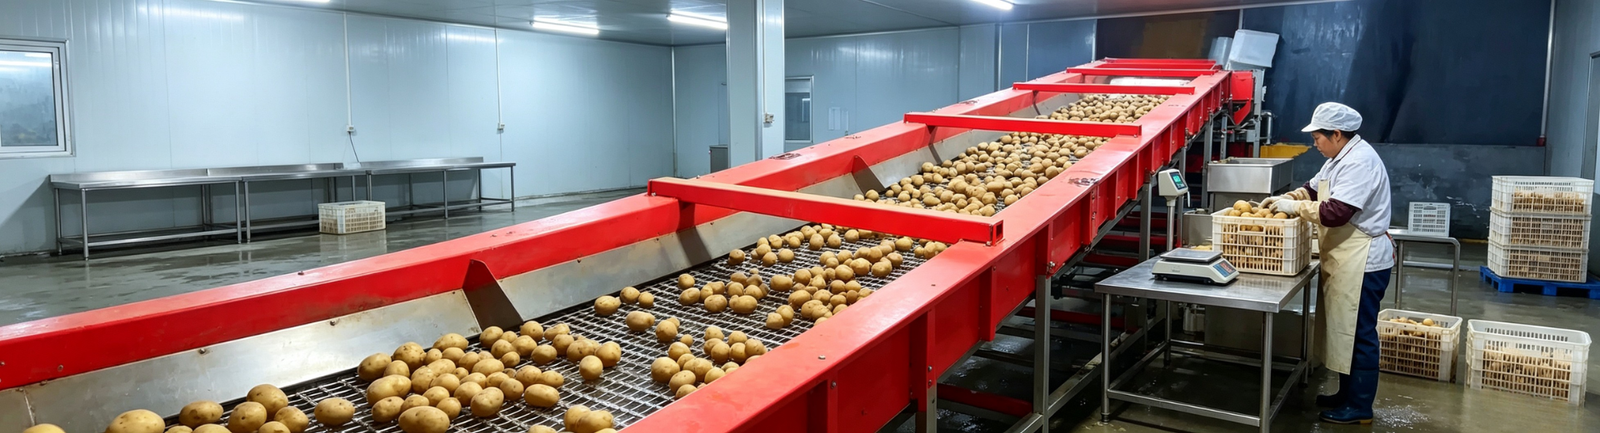
During potato harvest window, processing workshops face sudden raw‑material volume surges. High‑capacity potato inbound sorting equipment from Goldlocks stabilizes operation under peak‑load material inflow. Reinforced mechanical structure resists heavy‑duty continuous‑shift running. Pre‑shipment full‑load testing simulates harvest‑season working conditions to verify equipment reliability.
Southeast‑Asia countries push local rice‑processing industrialization to add value for domestic paddy output. More mill investors import Chinese complete rice‑milling turn‑key solutions for new‑plant construction or old‑factory renovation. Goldlocks accumulates multiple delivered rice‑mill project references across Laos, Myanmar, Vietnam and Cambodia for local customer reference.
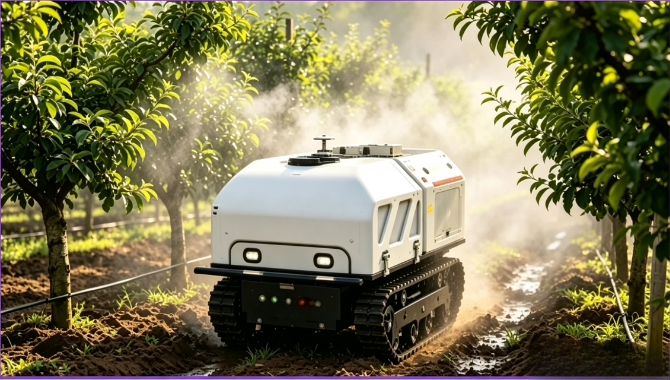
Orchard plant‑protection work faces labor shortage and harsh operating‑environment challenges. Our autonomous orchard spray robot uses Beidou RTK navigation for automatic route planning and precise pesticide spraying. The machine adjusts spray flow rate according to fruit‑tree canopy condition. Hybrid‑power design extends continuous working time inside hilly orchard sites across the world.
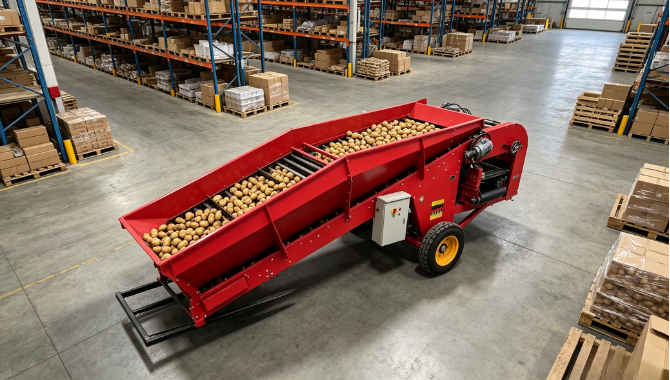
Emerging‑market potato growers are accelerating post‑harvest mechanization to cut heavy manual work. Chinese ISO‑certified potato sorting and washing equipment balances stable performance and competitive factory‑direct price. Goldlocks receives growing inquiries from Africa, Southeast Asia, Latin‑America clients for turn‑key potato processing plant construction projects.
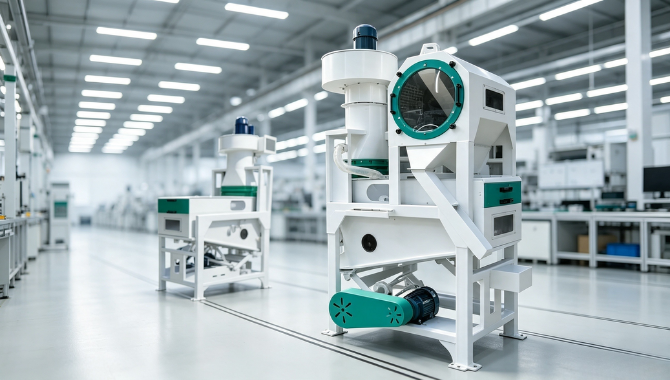
High‑quality seed preparation relies on reliable seed cleaner equipment to remove stones, debris, shriveled grains and foreign material. Goldlocks seed‑cleaning machinery serves seed‑breeding institutes and commercial seed producers. The unit finishes cleaning, destoning and preliminary grading before seed‑coating procedure. We customize sieve sets according to different grain physical parameters for global agricultural clients.
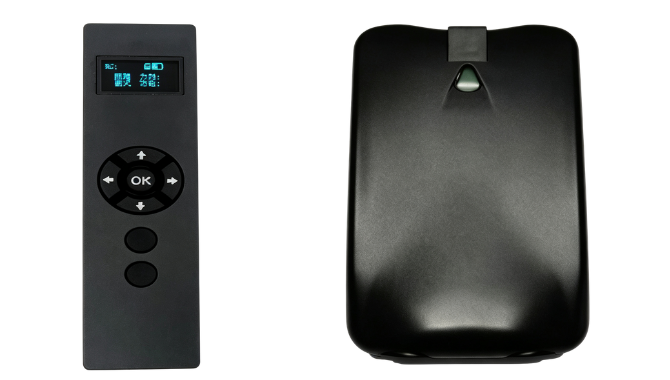
High‑precision navigation forms the core foundation for unmanned farm robots. Goldlock’s self‑developed Beidou RTK navigation controller offers centimeter‑grade positioning accuracy, supporting secondary‑development for research institutes and robot integrators. The unit adapts for orchard spray robot, lawn‑mowing robot and modular robot‑chassis platforms. Multiple communication interfaces simplify system integration work for global tech clients.
 English
 Русский
 Español
 Français
 Português
 Tiếng Việt